Double Spiral IQF Quick Freezer Machine Technology: The Ultimate Industrial Solution for Seafood & Frozen Food Plants to Minimize Drip Loss and Meet Global Export Standards
Critical Challenges in Indonesia's Frozen Food Processing Industry
The rapid expansion of seafood processing plants, poultry slaughterhouses, and ready-to-eat frozen food manufacturing across Indonesia demands increasingly stringent cold chain standards. Major export destinations such as the United States, the European Union, Japan, and China enforce strict regulations regarding organoleptic quality, microbiological safety, and net weight consistency for high-value commodities including vannamei shrimp, tuna loins, cephalopods, and value-added processed foods.
A persistent operational bottleneck eroding profit margins across industrial manufacturing zones—from Surabaya, Sidoarjo, Banyuwangi, and Makassar to Medan and Jakarta—is excessive dehydration loss (drip loss) caused by conventional static air blast freezers. When food products freeze slowly, water molecules within the cellular tissue form large, jagged ice crystals. These macro-crystals puncture and rupture cell membranes in meat and seafood. Consequently, when the product undergoes thawing at the consumer or industrial buyer level, nutrient- and protein-rich intracellular fluids leak out massively. The product becomes mushy, loses its natural freshness, suffers a net weight reduction of 3% to 5%, and frequently clumps together into solid blocks, severely hindering automated weighing and packaging lines.
To eliminate these technical and financial losses, transitioning to Individual Quick Freezing (IQF) technology is no longer merely a facility upgrade—it is a strategic imperative for processing plants pursuing operational excellence and international compliance certifications such as HACCP, BRCGS, and ISO 22000.
Why Double Spiral Quick Freezing Transforms Factory Competitiveness
The core physics behind successful IQF processing lies in maximizing the heat transfer rate as the product passes through the critical crystallization or nucleation zone—specifically when the core product temperature drops from minus 1 degree Celsius to minus 5 degrees Celsius. The faster a product traverses this thermal window, the smaller, finer, and more uniform the resulting intracellular ice crystals become.
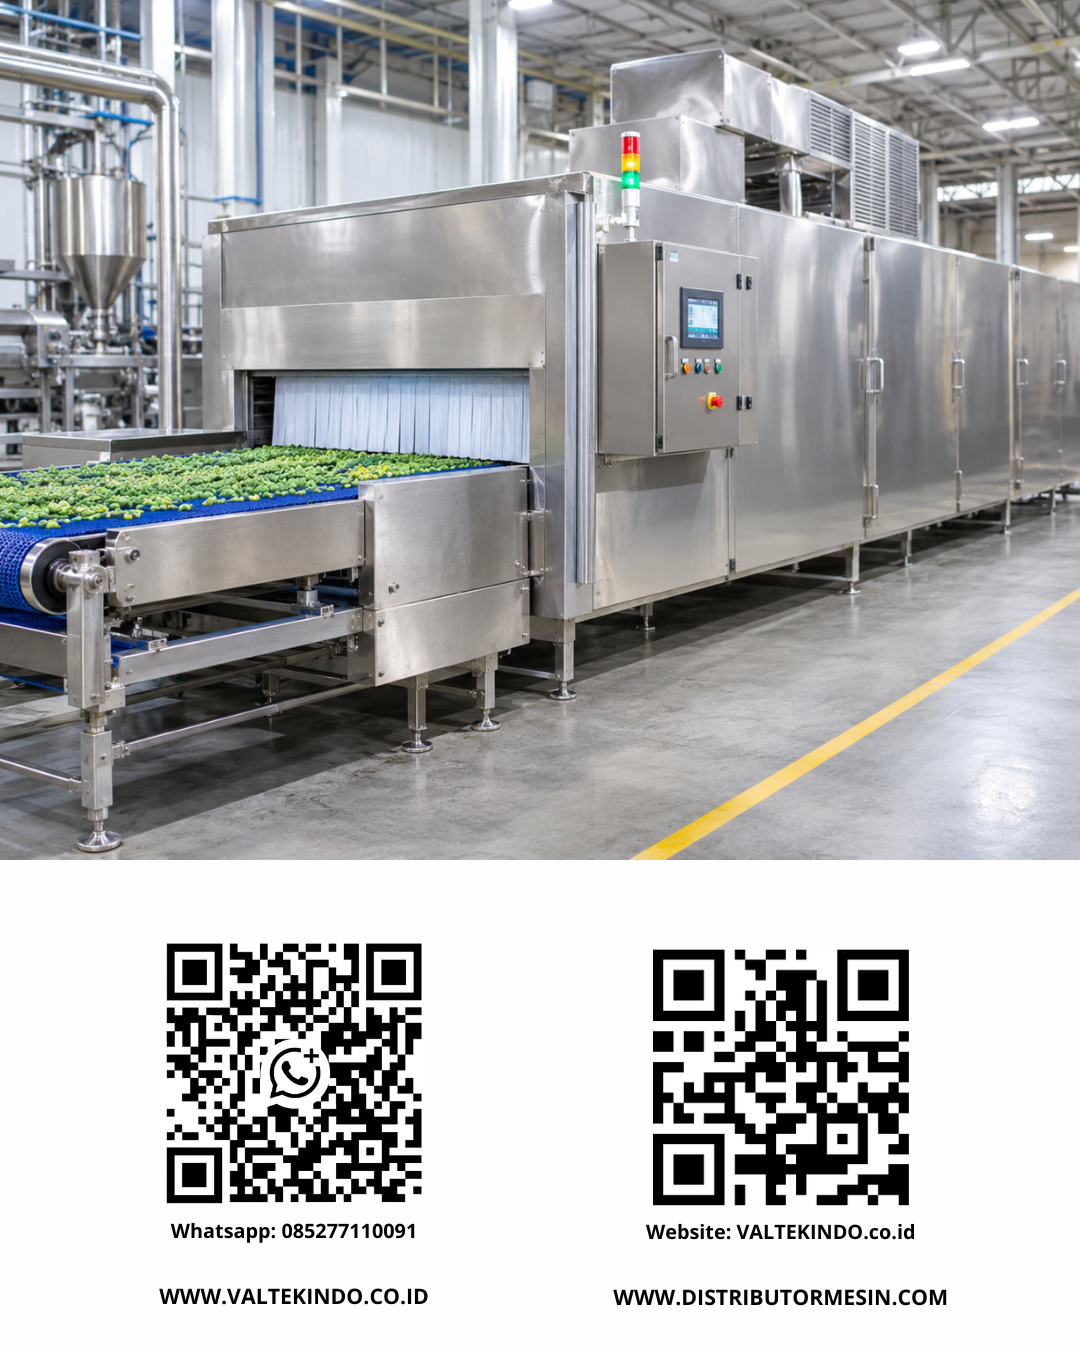
Unlike linear tunnel freezers that require massive horizontal floor space spanning dozens of meters, a Double Spiral configuration revolutionizes vertical space utilization. A continuous food-grade conveyor belt (modular plastic or stainless steel wire mesh) spirals upward around a primary rotating drum and spirals downward around a secondary drum within a single, fully insulated thermal enclosure. This advanced mechanical layout accommodates an exceptionally long freezing path within a compact factory footprint, delivering continuous in-line production capacities ranging from several hundred kilograms to multiple metric tons per hour.
Manufacturing plants planning cold storage modernization or production line scale-ups can seamlessly integrate the High-Capacity Energy-Efficient Double Spiral Individual Quick Freezer to ensure every individual piece of product—whether peeled deveined shrimp, poultry cuts, chicken nuggets, dim sum, meatballs, or diced tropical fruits and vegetables—freezes separately with zero clumping.
Engineering Specifications and Technical Advantages of the Double Spiral IQF Freezer
For Engineering Managers and Quality Assurance Directors, selecting an industrial IQF freezer requires rigorous evaluation of mechanical reliability, airflow thermodynamics, and sanitary construction. Below are the core engineering parameters that position the Double Spiral IQF system at the forefront of heavy-duty food processing:
- High-Velocity Symmetrical Airflow Aerodynamics: The evaporator system is precision-engineered to deliver pressurized, uniform cold airflow that sweeps evenly across every tier of the spiral belt. Heat exchange occurs symmetrically from both above and below the conveyor belt, generating an instant surface crust freeze within the first few seconds of product entry. This immediate crust freezing locks in internal moisture, effectively keeping dehydration loss below 0.5%.
- Full Food-Grade Stainless Steel Construction (SUS 304 / SUS 316L): All internal structural frames, drive drums, fasteners, and conveyor belts are fabricated from certified food-grade stainless steel capable of withstanding extreme sub-zero temperatures, high humidity, and rigorous daily chemical sanitation cycles. The enclosure features a seamless sloped floor with integrated drainage channels to prevent standing water and eliminate potential harborage points for pathogens such as Listeria or Salmonella.
- High-Density Polyurethane Insulated Enclosure Panels: The freezer cabin utilizes high-density polyurethane (PU) sandwich panels (exceeding 42 kg per cubic meter) with an optimal thickness of up to 150 mm, clad in stainless steel sheets on both sides and sealed via airtight cam-lock mechanisms. This superior thermal insulation eliminates thermal bridging and maintains stable internal operating temperatures between minus 35 degrees Celsius and minus 42 degrees Celsius.
- Intelligent Drum Drive System and Integrated PLC Automation: Spiral drum rotation speed, evaporator temperature, defrosting cycles, and automatic belt tension safety sensors are precisely governed through a Programmable Logic Controller (PLC) paired with an intuitive touchscreen Human Machine Interface (HMI). Operators can pre-program and store multiple freezing recipes tailored to varying product thicknesses and thermal loads, enabling rapid production changeovers with minimal downtime.
- Flexible Refrigeration Compatibility and Air Defrost Technology: The evaporator coils are fully compatible with industrial Ammonia ($NH_3$) systems, eco-friendly Freon refrigerants (R404A, R507), or $CO_2$ cascade refrigeration plants. Equipped with automated Air Defrost System (ADF) technology that continuously clears frost buildup from evaporator fins, the machine supports extended continuous operating shifts (18 to 22 hours non-stop) without thermal efficiency degradation.
Direct Financial Impact on Plant Profitability
Consider a practical financial simulation for a shrimp or poultry processing plant operating at a capacity of 2,000 kg per hour across a 16-hour daily shift (32,000 kg per day). If an outdated blast freezer causes a 3% dehydration weight loss, the factory loses approximately 960 kg of sellable product weight every single day purely due to moisture evaporation inside the freezing chamber. By upgrading to a Double Spiral IQF system that restricts moisture loss to under 0.5%, the plant retains over 800 kg of sellable product weight daily. Over a standard 300-day annual production calendar, this preserved product tonnage translates into billions of Rupiah in recovered revenue—dramatically accelerating the capital equipment payback period.
To ensure exact alignment between freezing capacity (from 500 kg/hour to over 3,000 kg/hour), existing factory floor layouts, and downstream automated packaging lines, partnering with an experienced industrial machinery supplier is vital. PT Valtekindo Global Intertek stands as Indonesia's premier industrial machinery distributor, delivering end-to-end engineering support ranging from pre-installation thermal calculations and global-standard IQF freezer supply to on-site commissioning, operator training, and guaranteed long-term spare parts availability.
Contact Our Sales Team Today
Looking for high-quality industrial machinery, factory automation solutions, or customized equipment for your business? Our experienced sales team is ready to help you find the right solution, provide technical consultation, and offer the best pricing.
Contact Our Official WhatsApp Sales Team:
- WhatsApp Sales 1: 085222110091
- WhatsApp Sales 2: 085277110091
Visit our official websites to explore our complete product catalog, machine operation videos, technical information, and exclusive offers:
PT. Valtekindo Global Intertek is your trusted partner for industrial machinery, processing equipment, recycling systems, laboratory instruments, and factory automation solutions. Contact us today for a free consultation and receive the best solution tailored to your business needs.
Admin
AuthorAdmin is a writer on the Valtekindo website, providing informative content about High Quality Industrial Machinery and Testing Machines.
Related post:
- Optimizing Liquid Production Lines with Automatic Liquid Filling & Capping Machines for Modern Industries
- Investment Feasibility Analysis of Commercial AAC Lightweight Block Plant Packages: CAPEX Efficiency and Accelerated ROI Strategies in Modern Construction
- Optimizing Pharmaceutical Production Lines Through High Speed cGMP Compliant Automatic Blister and Strip Packaging Machine Integration
Latest Articles:
- Optimizing Liquid Production Lines with Automatic Liquid Filling & Capping Machines for Modern Industries
- Investment Feasibility Analysis of Commercial AAC Lightweight Block Plant Packages: CAPEX Efficiency and Accelerated ROI Strategies in Modern Construction
- Optimizing Pharmaceutical Production Lines Through High Speed cGMP Compliant Automatic Blister and Strip Packaging Machine Integration
- Modern Manufacturing Efficiency Strategy: Optimizing Production Lines with Modular Product Systems to Boost Factory Flexibility in Indonesia
- The New Standard in Material Testing: Why a Precision Lab Pulverizer Machine is a Critical Investment for Modern Factories in Indonesia