Industrial Color Sorter Machine: Precision Optical Sorting Technology for Improved Production Efficiency
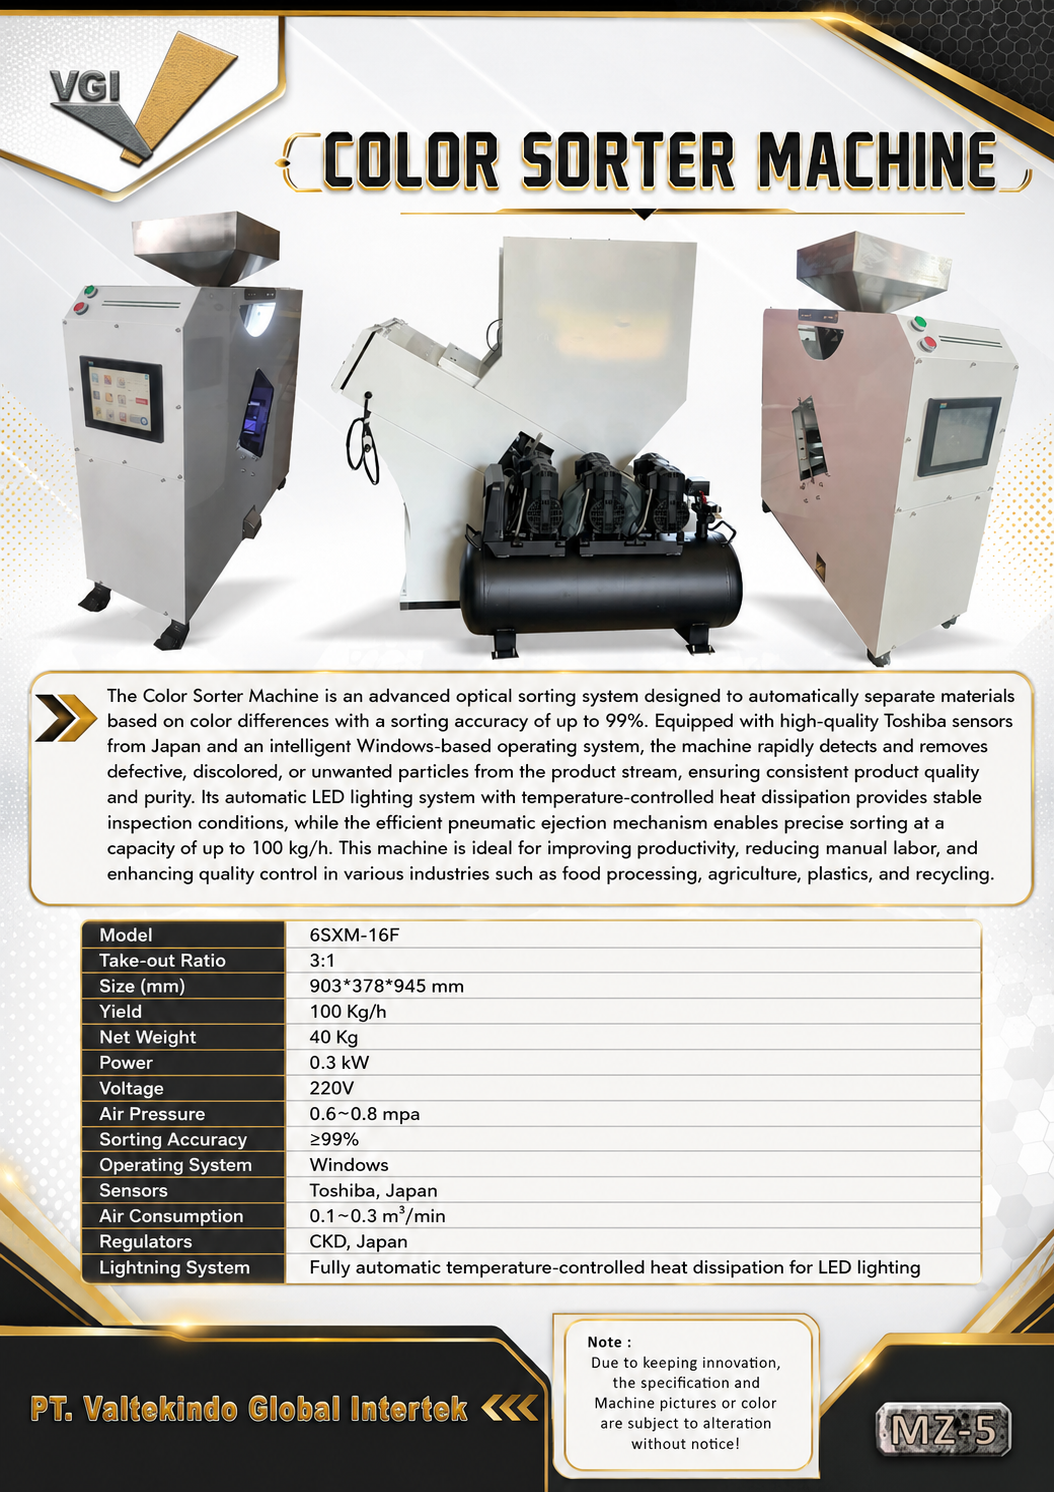 Click on the image to enlarge
FEATURE
DESCRIPTION / TECHNICAL SPECIFICATIONS
Enhance Your Quality Control Standards and Production Efficiency with an Automated Color Sorter Machine
In modern manufacturing and material processing industries, maintaining product purity and consistent quality is essential for staying competitive. Manual sorting processes are often time consuming, labor intensive, and prone to human error. The Color Sorter Machine is an advanced optical sorting system specifically engineered to automatically separate materials based on color differences with a sorting accuracy of ≥99%.
Core Functionality and Precision Operation This automated optical sorting machine rapidly detects and removes defective, discolored, or unwanted foreign particles from the main product stream. Equipped with high quality sensors from Toshiba (Japan) and pneumatic regulators from CKD (Japan), the system performs consistent visual inspections to ensure that only high grade materials move forward to the next processing or packaging stage.
Furthermore, the unit features a fully automatic temperature controlled heat dissipation system for its LED lighting. This maintains stable illumination conditions throughout continuous inspection operations. Paired with an efficient pneumatic ejection mechanism, the machine delivers precise material separation at a throughput capacity (yield) of up to 100 kg/h.
Key Advantages for Industrial Operations
- High Sorting Accuracy: Reliably separates materials based on subtle color variations with ≥99% accuracy and a 3:1 take out ratio.
- Reliable Japanese Components: Integrates Toshiba optical sensors from Japan and CKD regulators from Japan for dependable detection and operational longevity.
- Intelligent Operating System: Powered by a user friendly Windows operating system, allowing operators to easily configure parameters and monitor sorting performance.
- Stable LED Illumination: Fully automatic temperature controlled heat dissipation for the LED lighting system ensures consistent optical inspection stability.
- Energy Efficient and Compact Footprint: Operates on a low power consumption of 0.3 kW (220V) with a net weight of 40 kg and compact dimensions of 903 x 378 x 945 mm, making it easy to integrate into existing production lines.
- Efficient Pneumatic System: Operates smoothly within an air pressure range of 0.6 to 0.8 MPa and an air consumption rate of 0.1 to 0.3 m³/min.
Industrial Applications This optical color sorting machine is an ideal investment for improving productivity, reducing manual labor reliance, and strengthening quality control across multiple sectors, including:
- Food Processing Industry: Eliminates discolored, defective, or contaminated food particles to maintain strict food grade quality standards.
- Agriculture Sector: Sorts agricultural commodities and grains to achieve uniform appearance and high product purity.
- Plastics Manufacturing: Separates plastic pellets, flakes, or granules by color to ensure raw material consistency.
- Recycling Industry: Automatically sorts recycled material streams by color to maximize material recovery value and purity.
Consult Your Industrial Sorting Requirements with Us Upgrade the speed and precision of your quality control line with proven optical sorting technology. Contact our technical team today to request detailed specifications, discuss your material sorting applications, and receive a tailored quotation for your facility.
 Video
 Kontak Sales 1