Coal Crusher Feeder Machine Reliable Solution for Bulk Material Management
 Click on the image to enlarge
FEATURE
DESCRIPTION / TECHNICAL SPECIFICATIONS
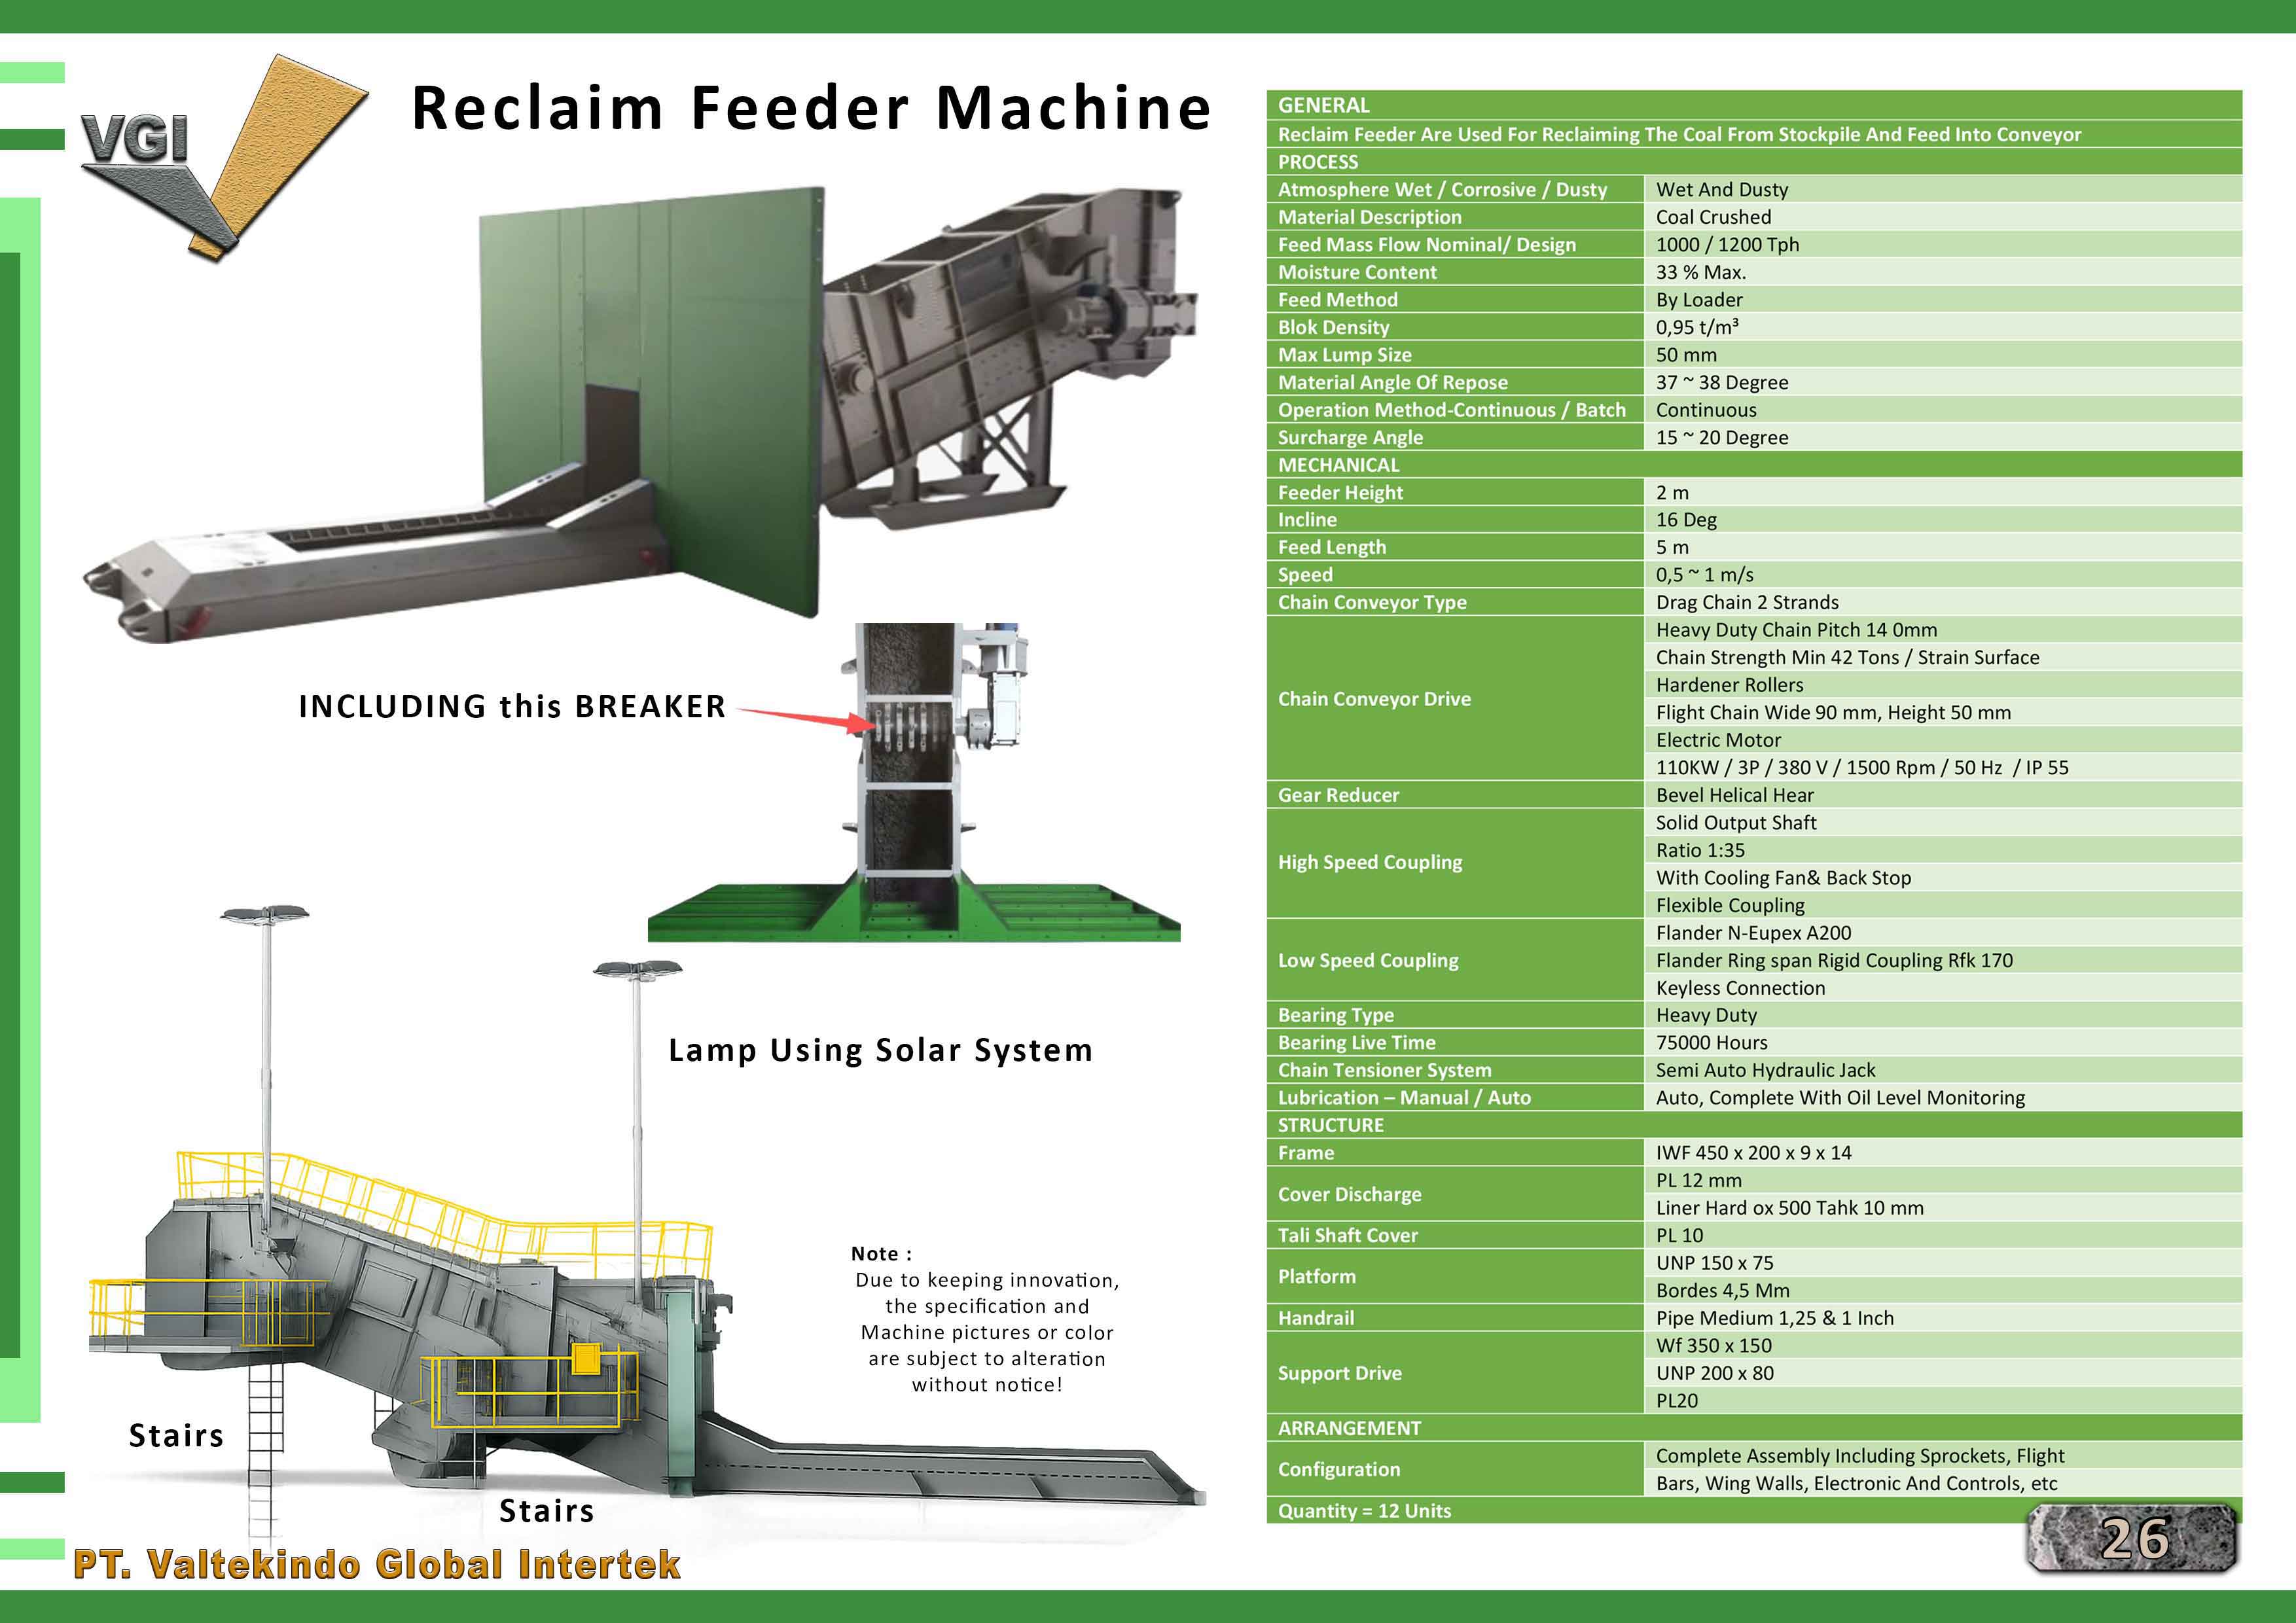
This is a premier solution for mining and bulk material handling operations. In the demanding world of heavy industry, operational efficiency begins with reliable material handling. This reclaim feeder machine is a precision-engineered solution designed for one primary purpose: to reclaim bulk materials, such as coal, from stockpiles and consistently feed them into conveyor systems. This equipment is engineered to be the backbone of your operation, ensuring a smooth, metered workflow. Designed to operate nonstop in a continuous mode, it eliminates costly bottlenecks and downtime, making it a vital asset for any mine site or processing facility.
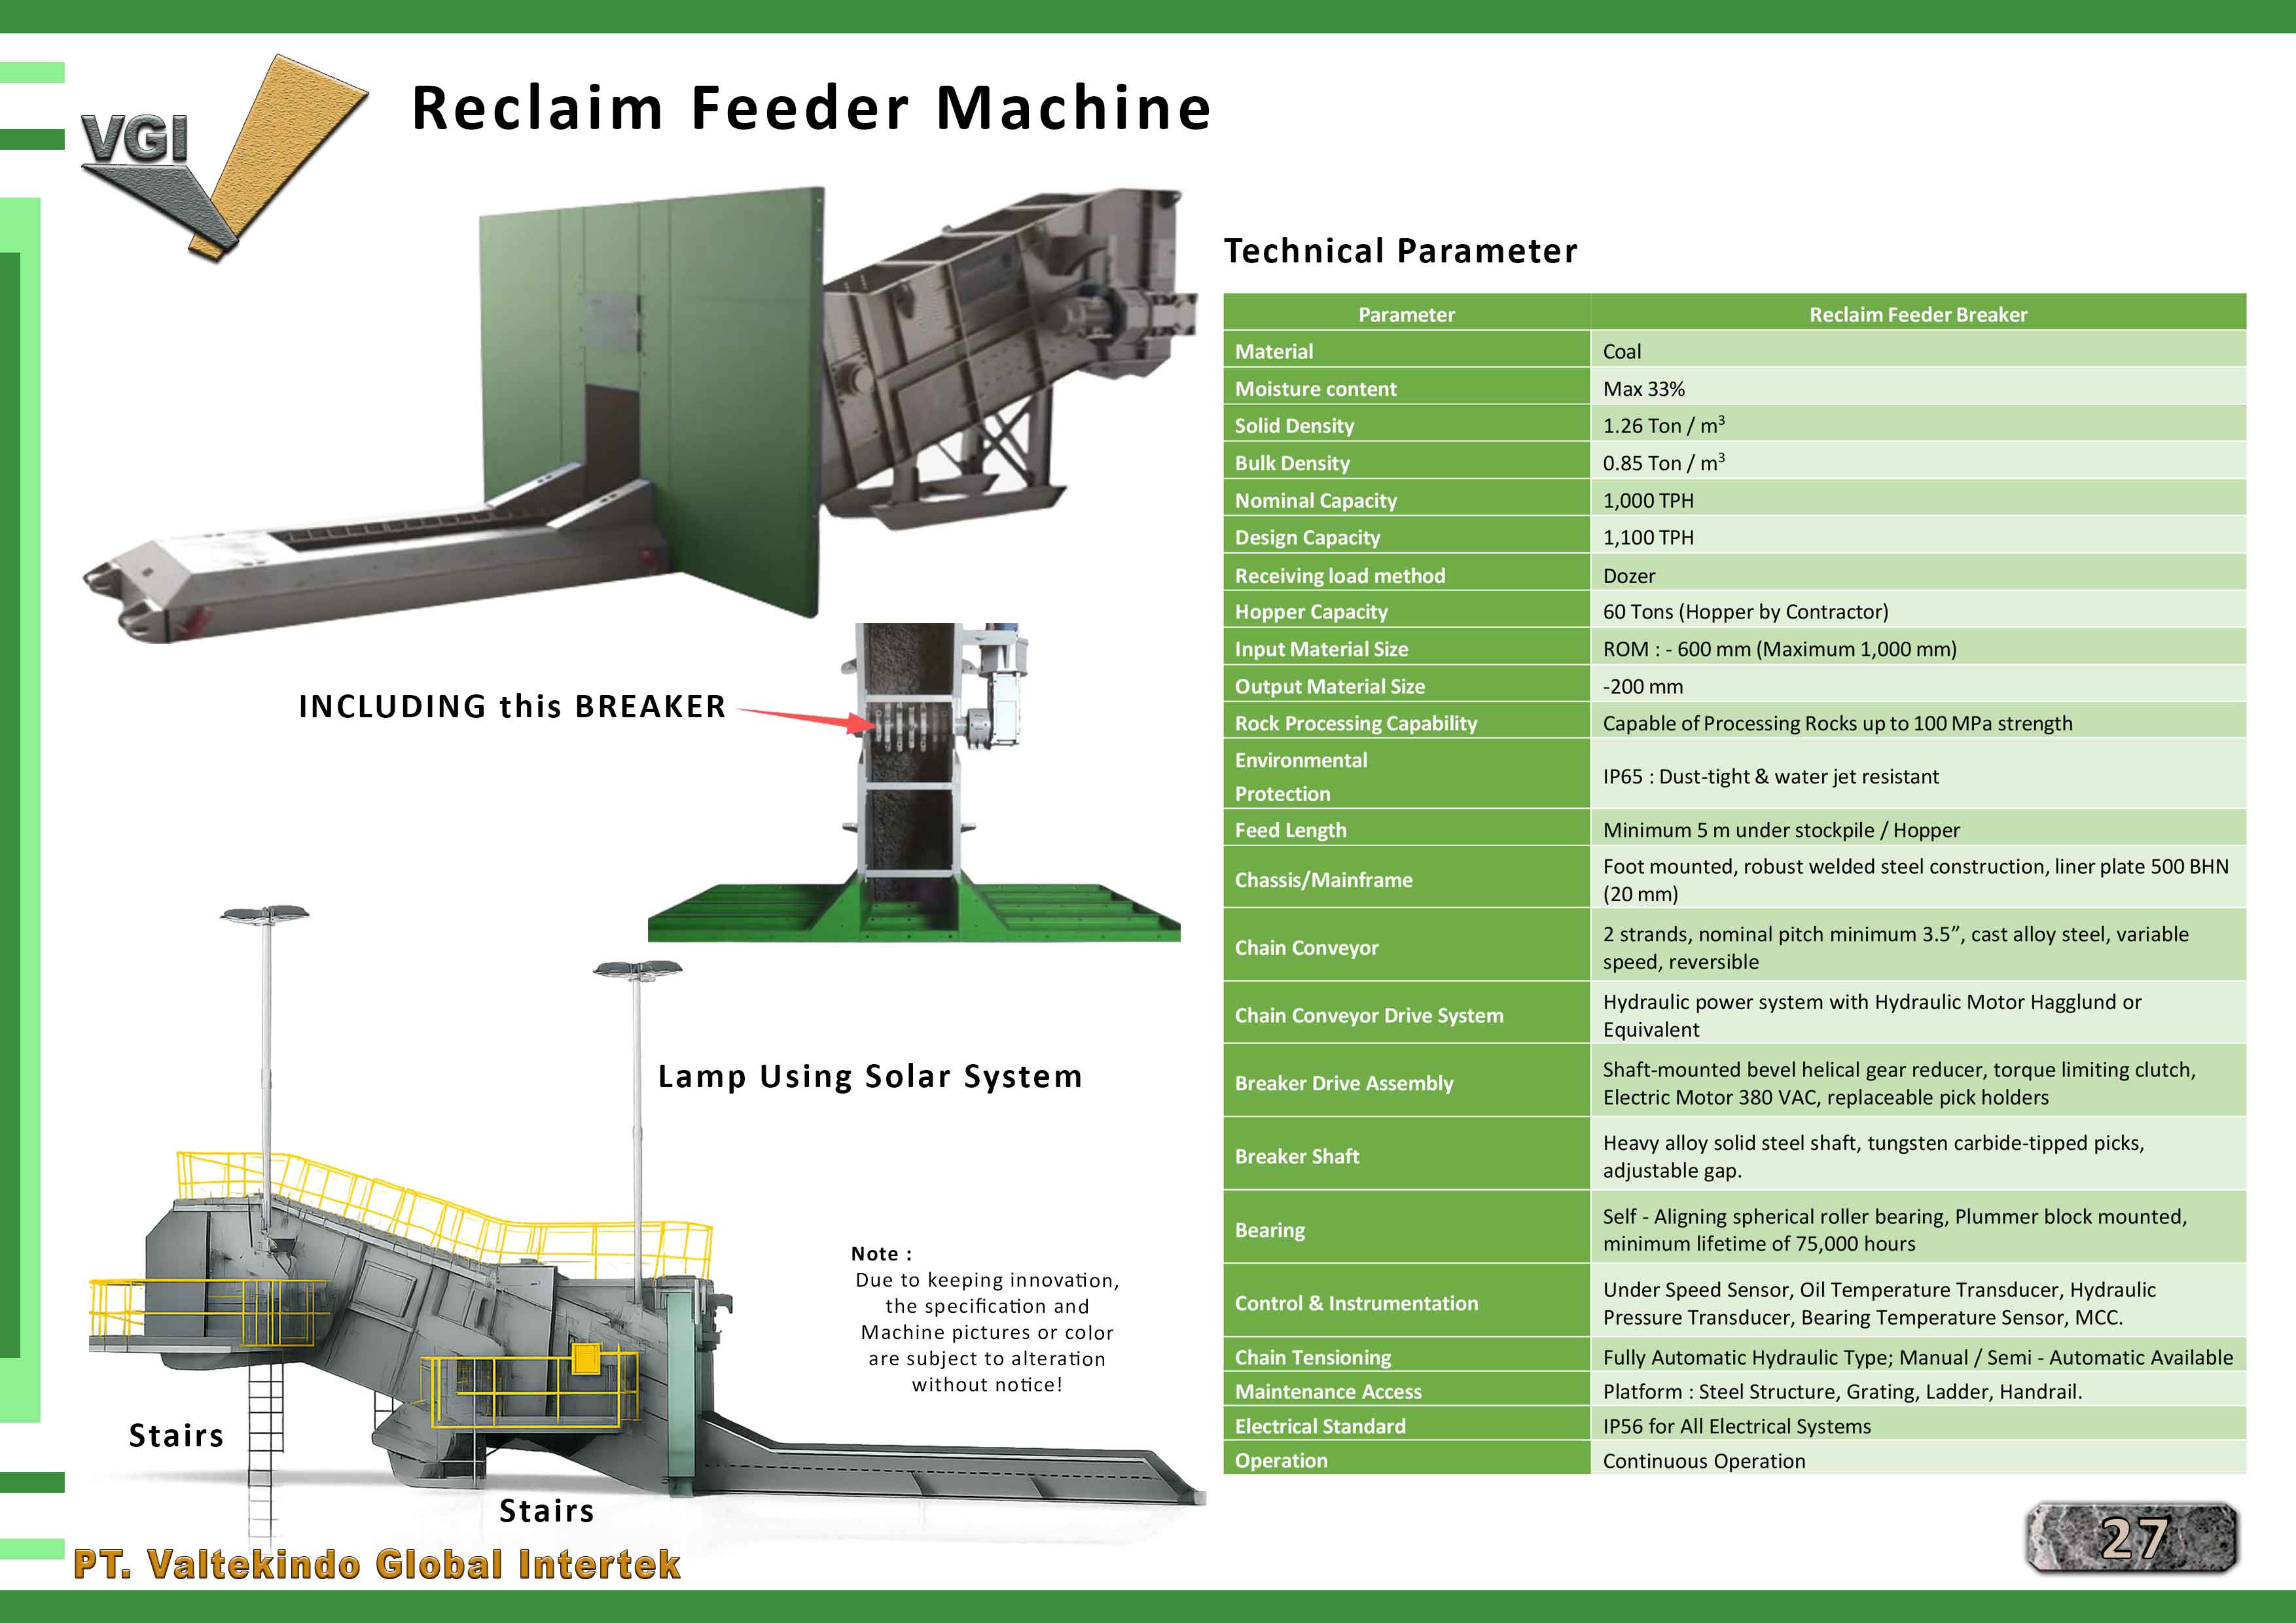
The core strength of this machine lies in its formidable capacity. With the ability to handle a design capacity of up to 1,100 or even 1,200 tons per hour (TPH), it is ready for large-scale operations. It is specifically optimized for materials like crushed coal and is capable of operating effectively even when the material has a very high moisture content, up to a maximum of 33%. Operational flexibility is also guaranteed, as the machine can be easily fed by either a dozer or a loader, adapting to your site's existing workflow.
For the most challenging applications, a variant equipped with an integrated breaker unit is available. This is not merely an add-on; it is a processing powerhouse. This breaker unit is capable of accepting raw (Run-of-Mine or ROM) material with massive lump sizes, up to a maximum of 1,000 mm. Its heavy alloy solid steel breaker shaft , armed with replaceable tungsten carbide-tipped picks , rotates with immense force, systematically crushing the large material down to a uniform, manageable output size of minus 200 mm. Even more impressively, the unit is engineered to process rocks with a strength of up to 100 MPa, turning the toughest material challenges into a processable product.
Durability is a fundamental design principle. Every component is built to last in the harshest environments, including wet, corrosive, and dusty atmospheres. The mainframe is a robust, welded steel construction , fortified with wear-resistant liner plates (such as Hardox 500 or 500 BHN) at 10 mm to 20 mm thickness to withstand relentless abrasion. The chain conveyor system itself is a testament to toughness, utilizing two strands of cast alloy steel chain or heavy-duty chain with a minimum strength of 42 tons.
Long-term reliability is secured by premium internal components. The machine employs heavy-duty self-aligning spherical roller bearings. These bearings, housed in plummer blocks , are rated for a minimum lifetime of 75,000 hours. This translates to years of uninterrupted operation, reducing the need for frequent and costly maintenance interventions. This reliability is at the heart of the machine's value proposition, ensuring maximum uptime for the user.
Advanced drive systems power this machine. The standard option includes a robust 110KW electric motor , paired with an efficient bevel helical gear reducer , complete with a back stop for operational safety. The breaker-equipped variant utilizes a sophisticated hydraulic power system. This hydraulic drive offers unparalleled control, allowing for variable speed and the ability to reverse direction (reversible). This feature is critical for managing difficult material flow and quickly clearing potential blockages, ensuring the operation keeps moving.
Smart maintenance and automation are key to efficiency. The machine is outfitted with an auto-lubrication system , complete with oil level monitoring, which ensures all critical points are perfectly lubricated without manual intervention. The chain tensioning system is also automated, using a fully automatic or semi-automatic hydraulic type, which maintains optimal chain tension at all times. Furthermore, a suite of advanced controls and instrumentation , including an under-speed sensor, oil temperature transducer, hydraulic pressure transducer, and bearing temperature sensors, provides real-time data for condition monitoring and predictive maintenance.
Engineered for total environmental resistance, the equipment features industry-leading protection. The entire unit is rated for IP65 environmental protection , meaning it is completely dust-tight and protected against low-pressure water jets. The electrical systems, including the control panels, are protected to an IP56 standard, ensuring safety and reliability even in wet conditions. Innovative features, such as lamps using a solar system, demonstrate a commitment to energy efficiency and sustainability. Personnel safety is also prioritized, with full maintenance access provided, including platforms, ladders, and handrails.
 Download
 Video
 Kontak Sales 1