The Importance of Vacuum Packaging Machines for the Coffee, Nut, and Granule Industries
In the increasingly tight competition of the food and beverage (F&B) and agricultural industries, product quality and freshness reign supreme. Modern consumers demand products of the highest standard, whether in terms of taste, aroma, or texture. For producers in the coffee, nut, and granule (such as spices, milk powder, or animal feed) industries, the biggest challenge is not the production process, but what happens after production: the packaging and storage process.
These three product categories—coffee, nuts, and granules—share one common enemy that is invisible yet incredibly destructive: air. Air, or more specifically the oxygen and moisture it contains, is the primary agent responsible for quality degradation. Oxidation, rancidity, clumping, and the loss of aroma are nightmares that can destroy a brand's reputation and cause significant financial losses.
This is where vacuum packaging technology emerges as the definitive solution. It is no longer just an option or an added value; it is a strategic necessity to protect product integrity from the factory to the consumer's hands. This article will delve deep into why a vacuum packaging machine is a vital investment for the coffee, nut, and granule industries, looking specifically at product challenges and the technological solutions available.
The Hidden Threat: Why Are Coffee, Nuts, and Granules So Vulnerable?
To understand the importance of vacuum packaging, we must first understand the unique nature of these three products and their vulnerability to the environment.
1. The Coffee Industry (Beans and Ground)
Coffee is a "living" product. After the roasting process, coffee beans release hundreds of volatile aromatic compounds that create the complex flavors we love. However, these compounds are extremely fragile.
- Oxidation and Aroma: Coffee's number one enemy is oxygen. Oxygen reacts with the oils and aromatic compounds in coffee, causing a rapid oxidation process. The result? The coffee becomes stale, loses its characteristic aroma, and produces a flat or rancid taste.
- Moisture: Coffee is hygroscopic, meaning it readily absorbs moisture from the air. Moisture can cause ground coffee to clump and accelerates the flavor degradation process.
2. The Nut Industry (Cashews, Almonds, Peanuts)
Nuts are known for their high content of healthy oils. Ironically, this nutritional advantage is their main weakness in storage.
- Rancidity: The vegetable oils in nuts are highly susceptible to lipid oxidation. Contact with oxygen causes the nuts to become rancid quickly. This process not only ruins the taste and smell but also destroys the product's nutritional value.
- Loss of Texture: Just like coffee, nuts also absorb moisture. This leads to the loss of the crunchy texture that characterizes high-quality nuts, making them soft or stale.
3. The Granule Industry (Spices, Milk Powder, Feed, Chemicals)
Products in powder or granule form, ranging from kitchen spices, formula milk, to bulk animal feed and agricultural chemicals, face a primary challenge with moisture.
- Caking: Moisture is the main cause of caking or clumping. A product that should be free-flowing becomes hard as a rock, ruining its functionality, making portioning difficult, and often rendering it unusable.
- Microbial Activity: Moisture creates an ideal environment for the growth of bacteria and fungi, which can spoil the product (especially animal feed or milk powder) and pose health risks.
The Vacuum Packaging Machine: The Definitive Quality-Locking Solution
A vacuum packaging machine operates on a simple yet highly effective principle: it removes almost all air (especially oxygen) from inside the packaging bag before sealing it hermetically (airtight). This process directly addresses all the problems mentioned above.
1. Completely Halting Oxidation By removing oxygen, the rate of oxidative reactions is suppressed to almost zero. For nuts, this means preventing rancidity. For coffee, it means locking in volatile aromatic compounds and preventing a stale taste.
2. A Barricade Against Moisture The hermetic seal created by the vacuum machine creates an impenetrable barrier against external moisture. This ensures that granular products remain dry and free-flowing, and nuts stay crunchy.
3. Drastically Extending Shelf Life By eliminating the two main destructive agents (oxygen and moisture), and inhibiting the growth of aerobic microorganisms, the product's shelf life can be extended significantly—often 3 to 5 times longer than conventional packaging methods.
4. Physical and Hygienic Protection Vacuum packaging "hugs" the product tightly, reducing movement and the risk of physical damage from impacts during transportation. Furthermore, the tight seal protects the product from external contaminants such as dust, insects, and dirt.
Choosing the Right Machine: Focusing on Industrial Scale
The theory of vacuum packaging is simple, but its execution on an industrial scale requires a machine that is reliable, robust, and specifically designed for heavy workloads. Coffee, nuts, and granules are often packaged in bulk volumes, ranging from 5 kg, 10 kg, to tens of kilograms. This is not a job for a household vacuum sealer.
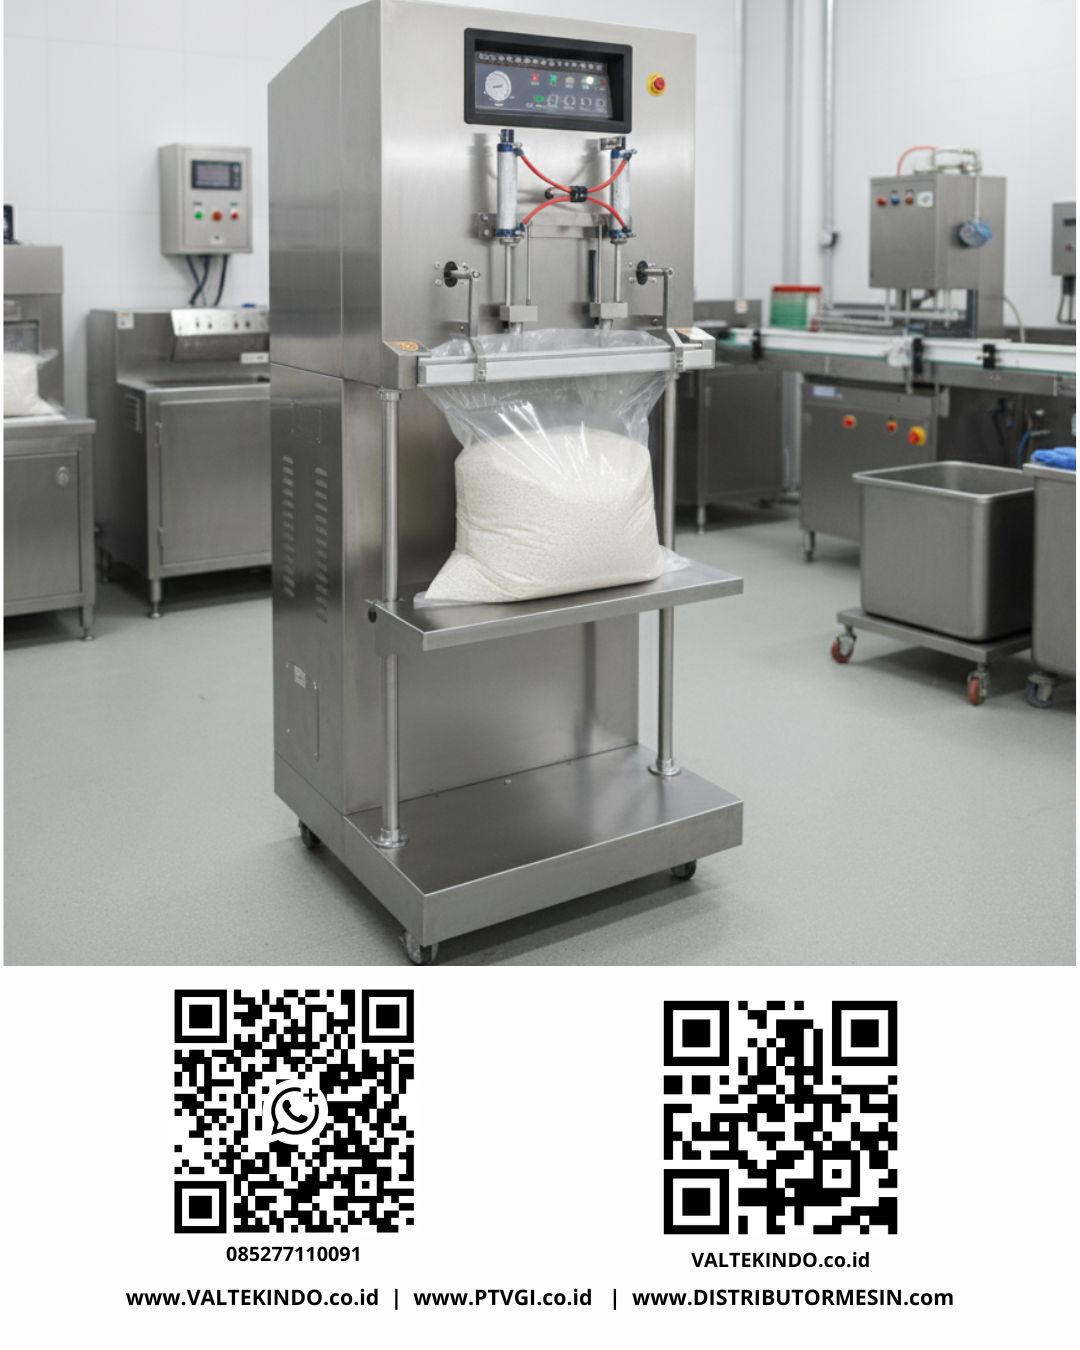
This is where machine specifications become crucial. As an example, let's look at the solutions offered by Valtekindo. For large-scale industrial needs, they provide a vertical vacuum packaging machine specifically designed to handle bulk and heavy products.
This machine has features that directly answer industrial needs:
- Heavy Load Capacity (up to 100 Kg): The vertical design and sturdy frame construction (machine weight of 220 Kg) allow it to handle large sacks or bags of coffee beans, rice, or animal feed without issue.
- Super Strong Seal (600 mm x 10 mm): For heavy packaging, the seal strength is everything. This machine uses an instant heating method with high power (1800 W) to create a 10 mm wide seal. This wide, strong seal is essential to prevent leaks in large packages.
- Powerful Vacuum Pump (0.75 kW): To draw air out of large bags filled with granules or beans, a powerful vacuum pump is required. This pump's strength ensures the optimal vacuum level is reached quickly.
- Production Efficiency (3-4 Cycles/Minute): In a factory environment, speed is money. This pneumatic-powered machine is designed for high throughput, keeping pace with a fast production line.
- Flexible Control: The ability to precisely set the vacuum time, sealing time, and cooling time is critical. Different products (e.g., freshly roasted coffee vs. cashew nuts) may require slightly different vacuum settings for optimal results.
Using a machine with specifications like this is no longer just about packaging; it's about adopting Advanced Vacuum Packaging Technology for Maximum Product Safety and Quality. It is an investment that guarantees the premium quality you create in your production facility is the same quality your end customer receives.
Conclusion: A Vital Investment for Competitive Advantage
For the coffee, nut, and granule industries, vacuum packaging is no longer a luxury. It is the front line in the war against oxidation, moisture, and rancidity. Ignoring this technology is tantamount to letting your product quality, brand reputation, and potential profits be eroded by thin air.
Adopting the right industrial vacuum packaging machine—one that can handle large volumes, provide a strong seal, and operate efficiently—is a strategic move to reduce product spoilage, expand distribution reach, and win consumer trust.
Don't let your superior product quality degrade simply because of inadequate packaging. It's time to switch to a professional vacuum packaging solution.
Optimize Your Industry Today!
Achieve production efficiency and the highest quality standards with a trusted industrial machinery provider. Explore our wide selection of premium processing and testing equipment at:
Website : valtekindo.co.id
Wesbite : distributormesin.com
Consult your technical needs with our expert sales team:
WhatsApp 1: +62 852-2211-0091
WhatsApp 2: +62 852-7711-0091
Admin
AuthorAdmin is a writer on the Valtekindo website, providing informative content about High Quality Industrial Machinery and Testing Machines.
Related post:
- Pharmaceutical Factory Production Escalation Strategy: Why Investing in an Automatic Capsule Filling Machine is the Most Crucial Business Decision
- High-Precision Wire Cut EDM Technology in 2026: The Ultimate Solution for Mold Making, Stamping Dies, and Automotive Component Fabrication Without Thermal Distortion
- 2026 Automated Carton Sealer & Erector Investment Guide: End-of-Line Automation Strategies for Industrial Plant Efficiency