Waste Processing Revolution: SRF Production Plant Gen 3 with Smart Sorting & Maximum Efficiency
 Click on the image to enlarge
FEATURE
DESCRIPTION / TECHNICAL SPECIFICATIONS
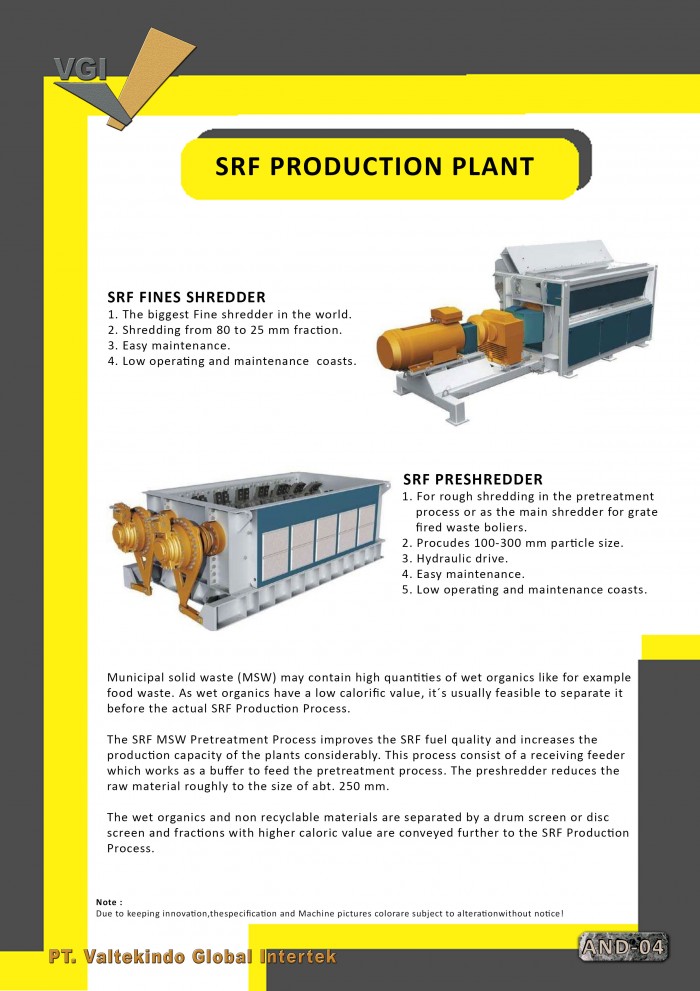
Enter a new era of sustainable waste management with the Generation 3 Solid Recovered Fuel (SRF) production system. This solution is engineered to transform municipal solid waste (MSW), commercial waste, and scrap tires into high-quality, clean fuel with high calorific value. The plant features the world’s strongest SRF Shredder, capable of reducing any material to a uniform particle size in a single phase, eliminating the need for secondary shredding. Equipped with a Massive Impact Protection System, the machine automatically rejects un-shreddable objects to protect internal components, ensuring low maintenance costs.
Separation efficiency is maximized through the SRF Fines Screen, which utilizes rotating shafts to precisely separate sand, soil, glass, and heavy metals. Ferrous metals are removed by belt magnets, while conductive metals like aluminum are separated by eddy current separators. The final product is a high-grade "light fluff" ready for use in power boilers and cement kilns. The entire facility can be integrated with hybrid solar panel systems and lithium battery storage to achieve total energy independence via smart smartphone monitoring. For field operations, we also offer DTH Drill Rigs with a 300-meter drilling capacity, alongside Shaking Table and Spiral Chute technologies for maximum mineral recovery precision.
 Download
 Video
 Kontak Sales 1