Sell Industrial Reverse Osmosis Systems – Clean & Hygienic Water Treatment Solution
 Click on the image to enlarge
FEATURE
DESCRIPTION / TECHNICAL SPECIFICATIONS
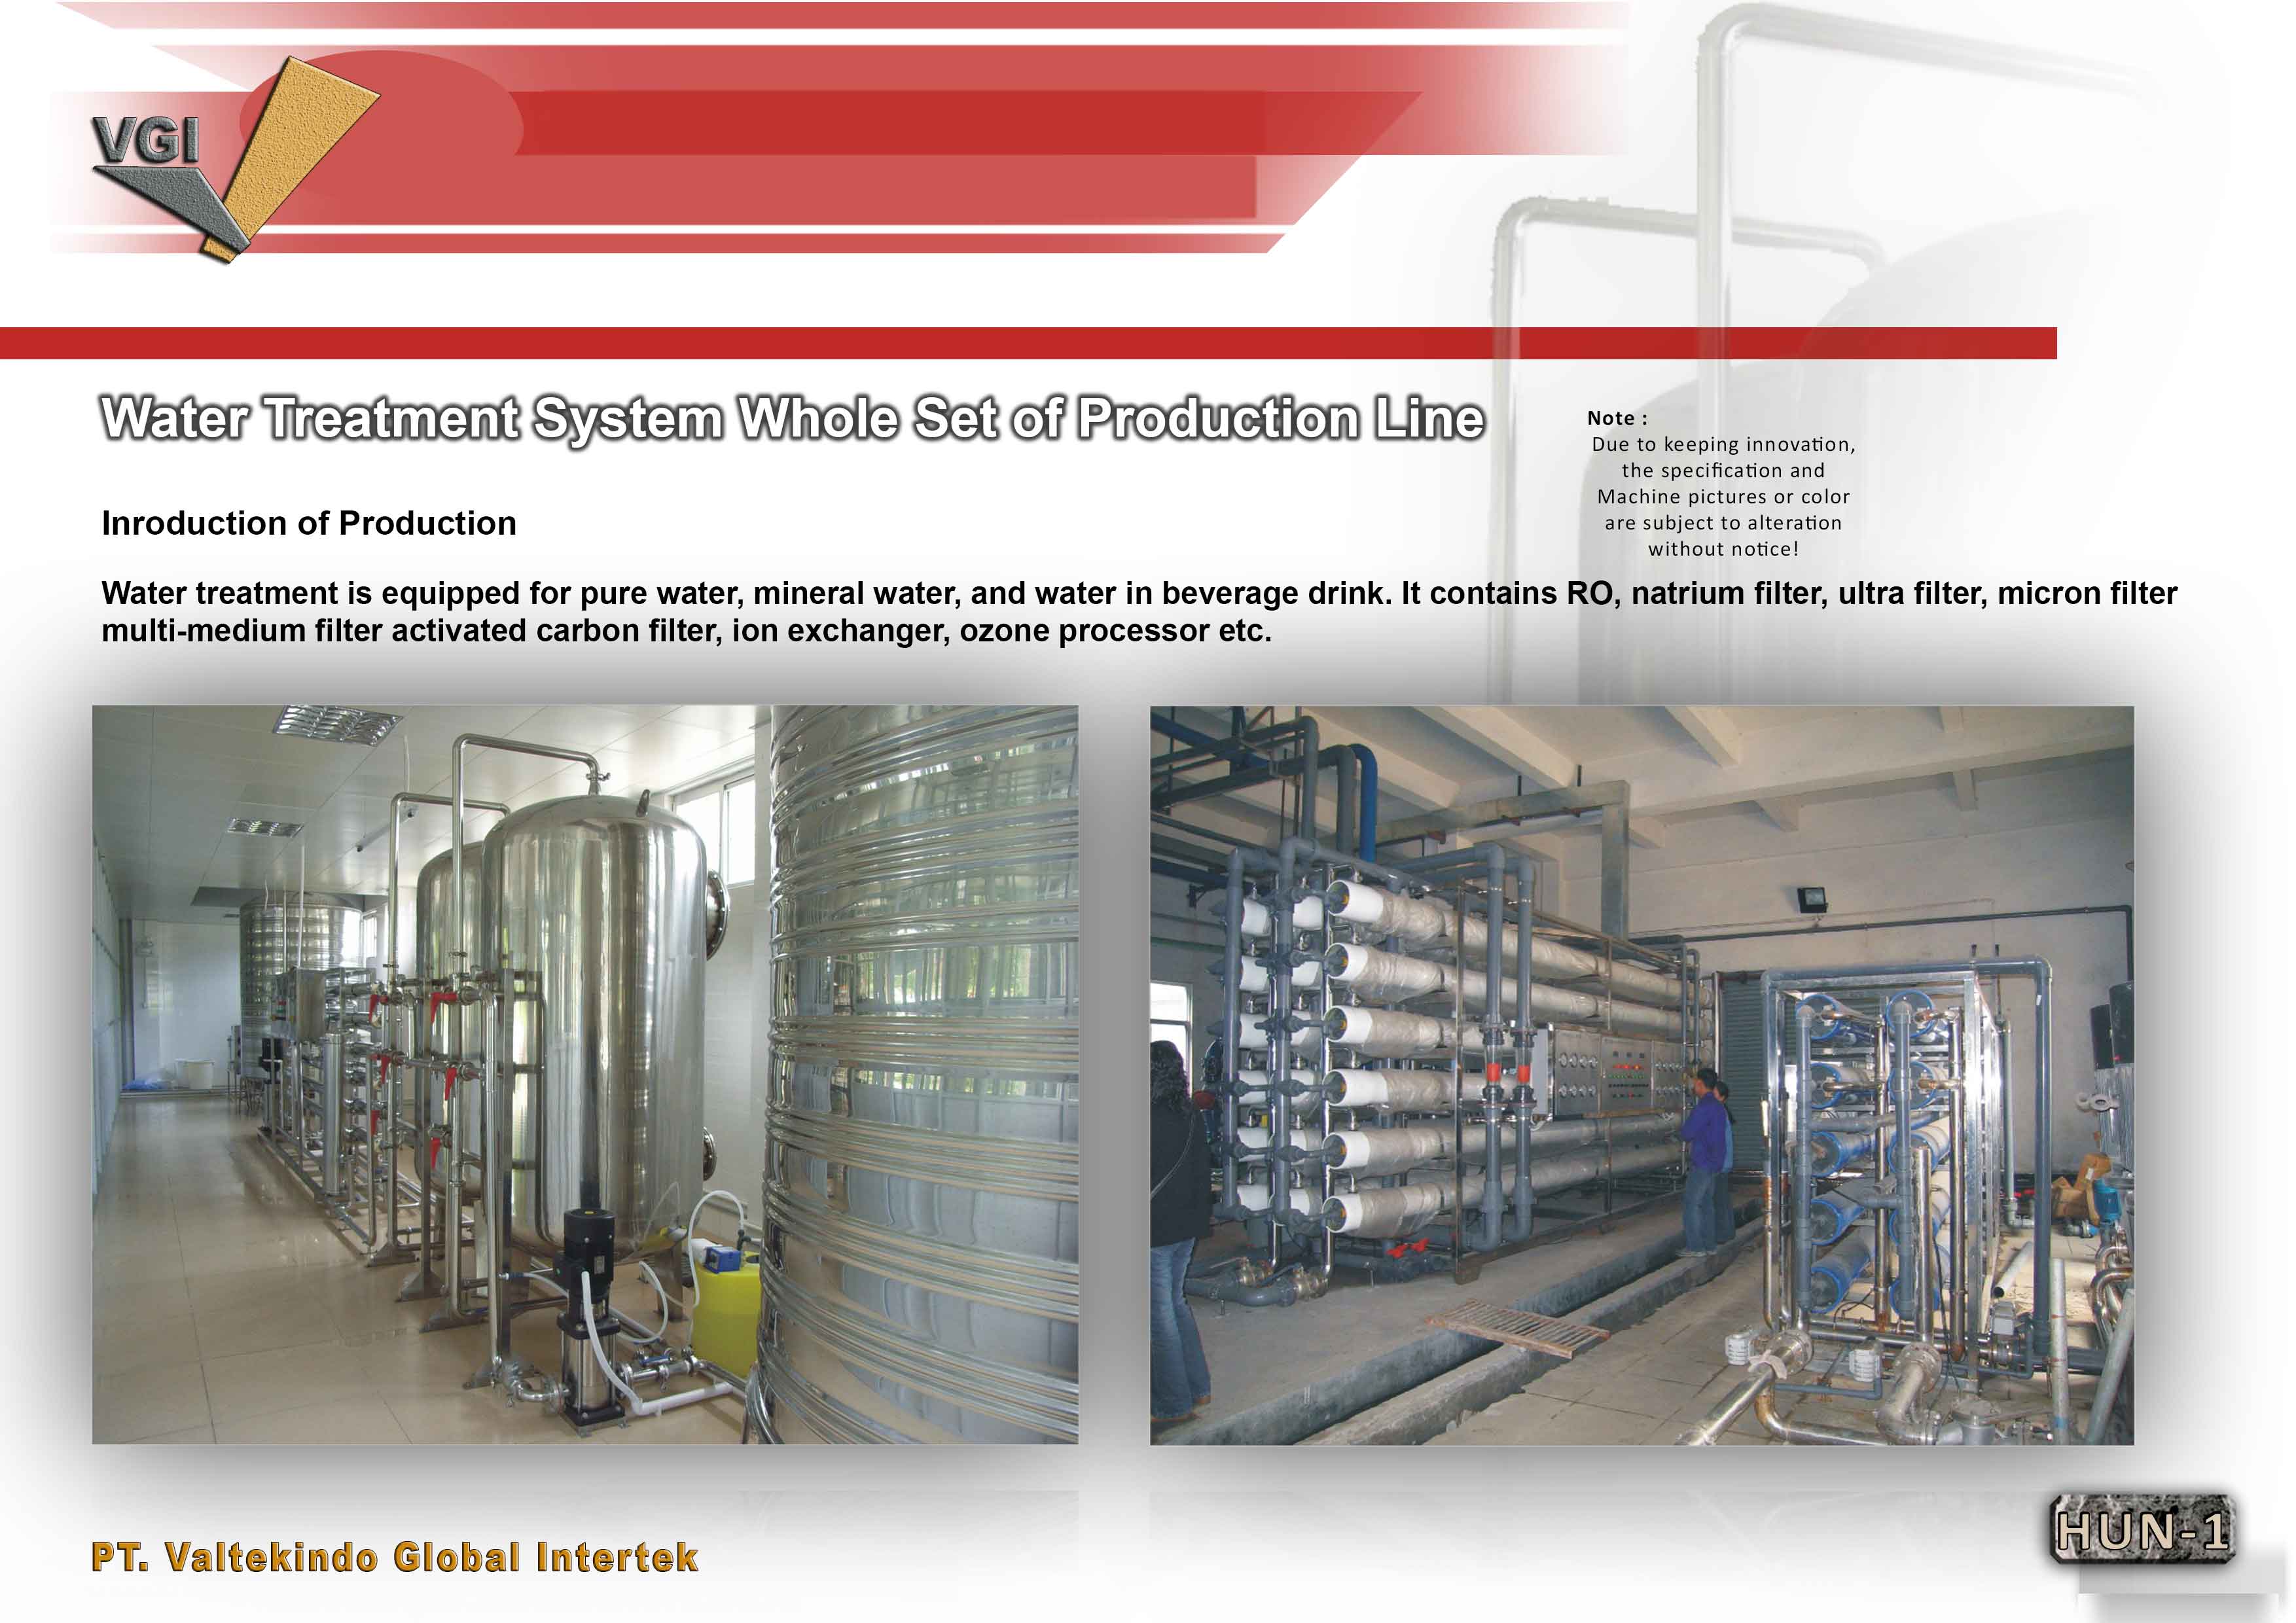
Achieve the highest standards of water purity for your industrial operations with our cutting edge Reverse Osmosis (RO) systems. This technology is specifically engineered to meet the critical demands for high quality water in beverage and beer manufacturing, bottled mineral water production, pharmaceuticals, and electronics sectors. The system operates comprehensively through a highly effective multi stage filtration sequence. The process begins with mechanical filtration and active carbon filters to eliminate coarse particles, sediments, and undesirable odors.
The core strength of this system lies in its one stage or two stage osmosis purification technology, capable of producing water with exceptional purity levels. To ensure total hygiene and consumption safety, our equipment is featured with dual sterilization capabilities using ozone and UV light technologies, effectively eradicating germs and bacteria. Supporting components like ion exchange softening devices ensure the water is free from mineral hardness that could damage other production machinery. With a robust machine structure, efficient high pressure pumps, and food grade stainless steel storage tanks, this system guarantees a stable clean water supply for large scale factory operations with simplified maintenance.
 Video
 Kontak Sales 1